


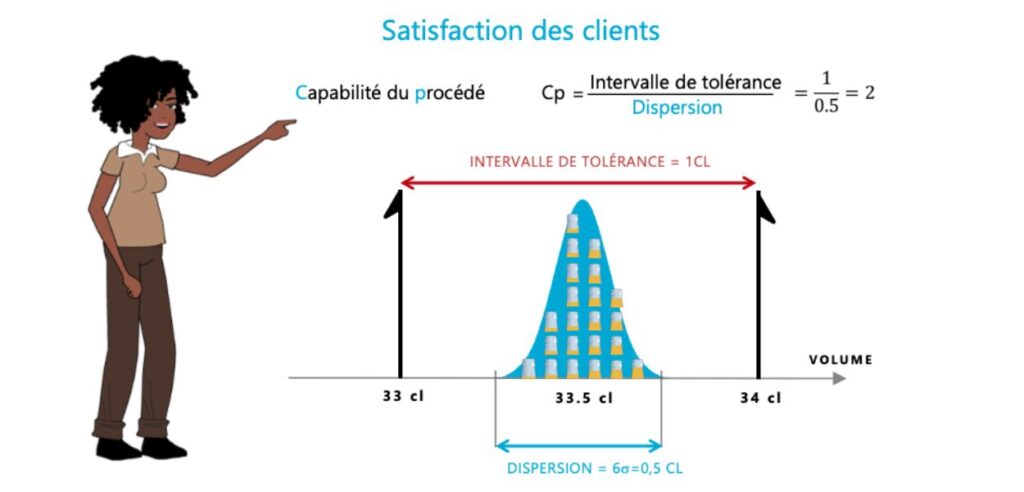
Can your process meet the tolerance?
Before beginning mass production, every quality team must answer a fundamental question: Is my process physically capable of producing within specifications? This is not a matter of adjustment or alignment—it is a matter of raw potential. This is precisely what the Cp index addresses—one of the most widely used metrics in statistical process control (SPC). But like any summary metric, it has specific limitations that must be understood to avoid drawing erroneous conclusions.
What the Cp Actually Measures
The Cp, or process capability index (Process Capability), compares the tolerance range defined by the engineering department with the actual variation measured in the process. The formula is simple:
Cp = (LSS − LSI) / (6σ)
where LSS is the upper specification limit, LSI is the lower specification limit, and 6σ represents the range of natural variation in the process (i.e., ±3 standard deviations around the mean).
In practical terms: if your tolerance is twice as wide as your process variation, the Cp is 2.0. If they are identical, the Cp is 1.0—and statistically, approximately 0.27 % of your production will fall outside the tolerance, even under the best conditions.
The most commonly used industrial standard is Cp ≥ 1.33, which corresponds to a tolerance at least 1.33 times wider than the process variation. In demanding industries such as the automotive and aerospace sectors, a threshold of 1.67 or even 2.0 is often required.
Calculation criteria: an often-overlooked limitation
The Cp is calculated in short-term terms, that is, on a sample taken during an initial capability study, under deliberately stabilized conditions: same operator, same material batch, same settings. The objective is to evaluate the process’s intrinsic potential, free from sources of variation associated with the actual production environment.
This is both its strength and its weakness. Under ideal conditions, the Cp provides an upper bound on what the process can achieve. However, it does not reflect what will happen once the process is launched into long-term production, with tool changes, variations in raw material batches, shift rotations, or thermal drifts. These real sources of variation are simply not captured in the calculation.
The "Centering Trap": When a Good Cp Hides Poor Parts
This is the point that is most often misunderstood in the field. A high Cp simply means that The process variation is small relative to the tolerance. It says absolutely nothing about the position of this dispersion relative to the nominal target.
Imagine a tolerance of 10 ± 0.5 mm and a process whose natural variation spans 0.6 mm. The Cp is greater than 1.33—which appears satisfactory. But if the process is centered at 10.4 mm instead of 10.0 mm, a large proportion of the parts will exceed the upper specification limit, despite a good Cp.
The index exists precisely to address this reality Cpk, which takes into account both dispersion and deviation from the target. A well-controlled process should exhibit both a satisfactory Cp and a satisfactory Cpk. A significant difference between the two is a warning sign: the process has potential, but it is poorly centered.
How to Use the Cp Rigorously
To use this index effectively, there are a few practical rules to follow:
- Check for stability before performing the calculation. A CP calculated based on an unstable process (where special causes have been detected on a control chart) has no statistical significance. Stability is a prerequisite, not an option.
- Never interpret it on your own. Always consider Cp and Cpk together. A Cp ≥ 1.33 with a Cpk ≥ 1.33 indicates a capable process and Centered. A Cp ≥ 1.33 with a Cpk < 1.00 indicates a setup issue that must be corrected immediately.
- Plan ahead for the transition to mass production. A favorable short-term study does not guarantee long-term performance. Schedule a reassessment of capability (using Pp and Ppk, calculated based on long-term data) after the first few weeks of production.
- Ensure that the sample is representative. The recommended minimum sample size is 30 to 50 consecutive samples taken under uniform conditions.
CP is a powerful diagnostic tool, provided you ask it the right question: Does this process have the dimensional capability to meet the tolerance? To determine whether it actually performs this way under production conditions, we’ll need to look further—using Cpk for centering and Ppk for long-term performance. Together, these three metrics form a coherent capability dashboard, which no one should interpret in isolation.